Loading…
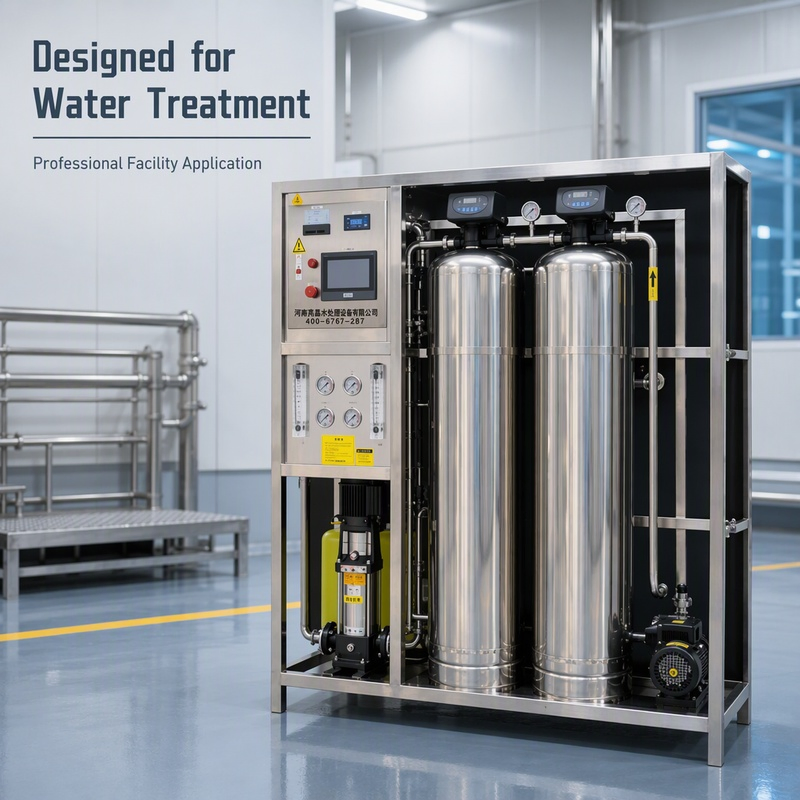
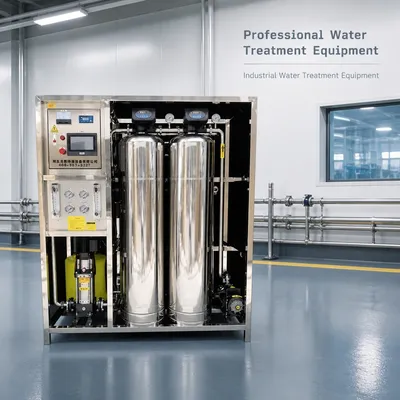
Reverse Osmosis Water Filter System for Bagged Water Factories with CE and RoHS Certification Stainless Steel Equipment
InStock Source-listed auditby Henan Zhonghai Environmental Protection Equipment Co., Ltd.
₹1,79,525≈ $2,150 · indicative, confirm with supplier
Description
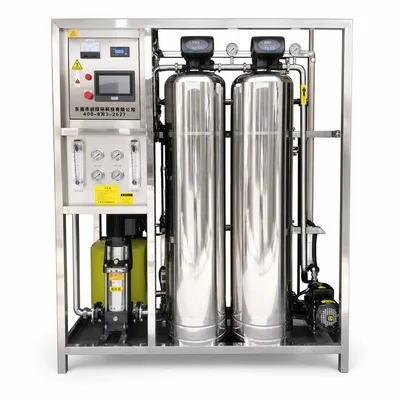
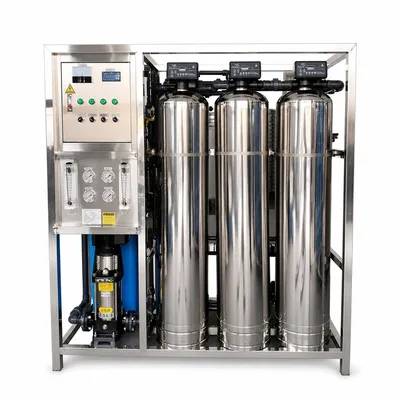
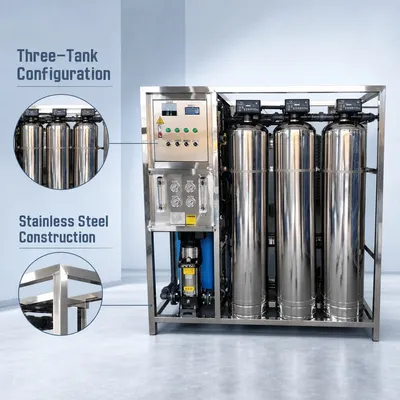
Reverse Osmosis Water Filter System for Bagged Water Factories with CE and RoHS Certification Stainless Steel Equipment. All pipes, joints and fittings are fabricated from 304/316L sanitary stainless steel, featuring acid & alkali resistance and anti-corrosion performance. No harmful solvent residues or leachates exist. Stainless piping delivers high tensile and compressive strength and pairs with dedicated high-pressure clamp flanges for reliable sealing under continuous heavy duty. A multi-grade quartz sand bed intercepts sediment, colloids and coarse particles in stages the first physical barrier of the system. High-iodine-value carbon rapidly adsorbs free chlorine, odour, humic substances and heavy metals, removing irreversible oxidative damage to the membrane. Food grade cation resin exchanges Ca and Mg, with an intelligent brine tank performing timed regeneration, keeping feed hardness low and removing the risk of inorganic scaling. A stainless steel security filter with a 5-micron high-precision cartridge forms the final safety net before the membrane, protecting the vertical multistage pump and the elements. complete train of sand, carbon, softening and fine filtration holds feed SDI below 5, keeping the membrane at design conditions and clearly reducing replacement frequency and O&M cost. The stainless system withstands heat and corrosion, supporting acid, caustic and hot-water CIP to restore membrane flux and system hygiene without dismantling. Branded high-rejection RO elements with precise pre-treatment deliver stable 98-99.3% salt rejection, removing dissolved salts and heavy metals. High-sensitivity stainless pressure sensors and solenoid valves provide low-inlet-pressure shut-down and over-pressure interlock, with automatic start/stop and audible-visual alarm.
Specifications
TypeReverse Osmosis Filtration
UsageDrinking Water Treatment Plant
Model NO.Stainless steel 2000L RO water filter
Product NameWater Treatment System Processing Reverse Osmosis
CertificationCE, RoHS