Loading…
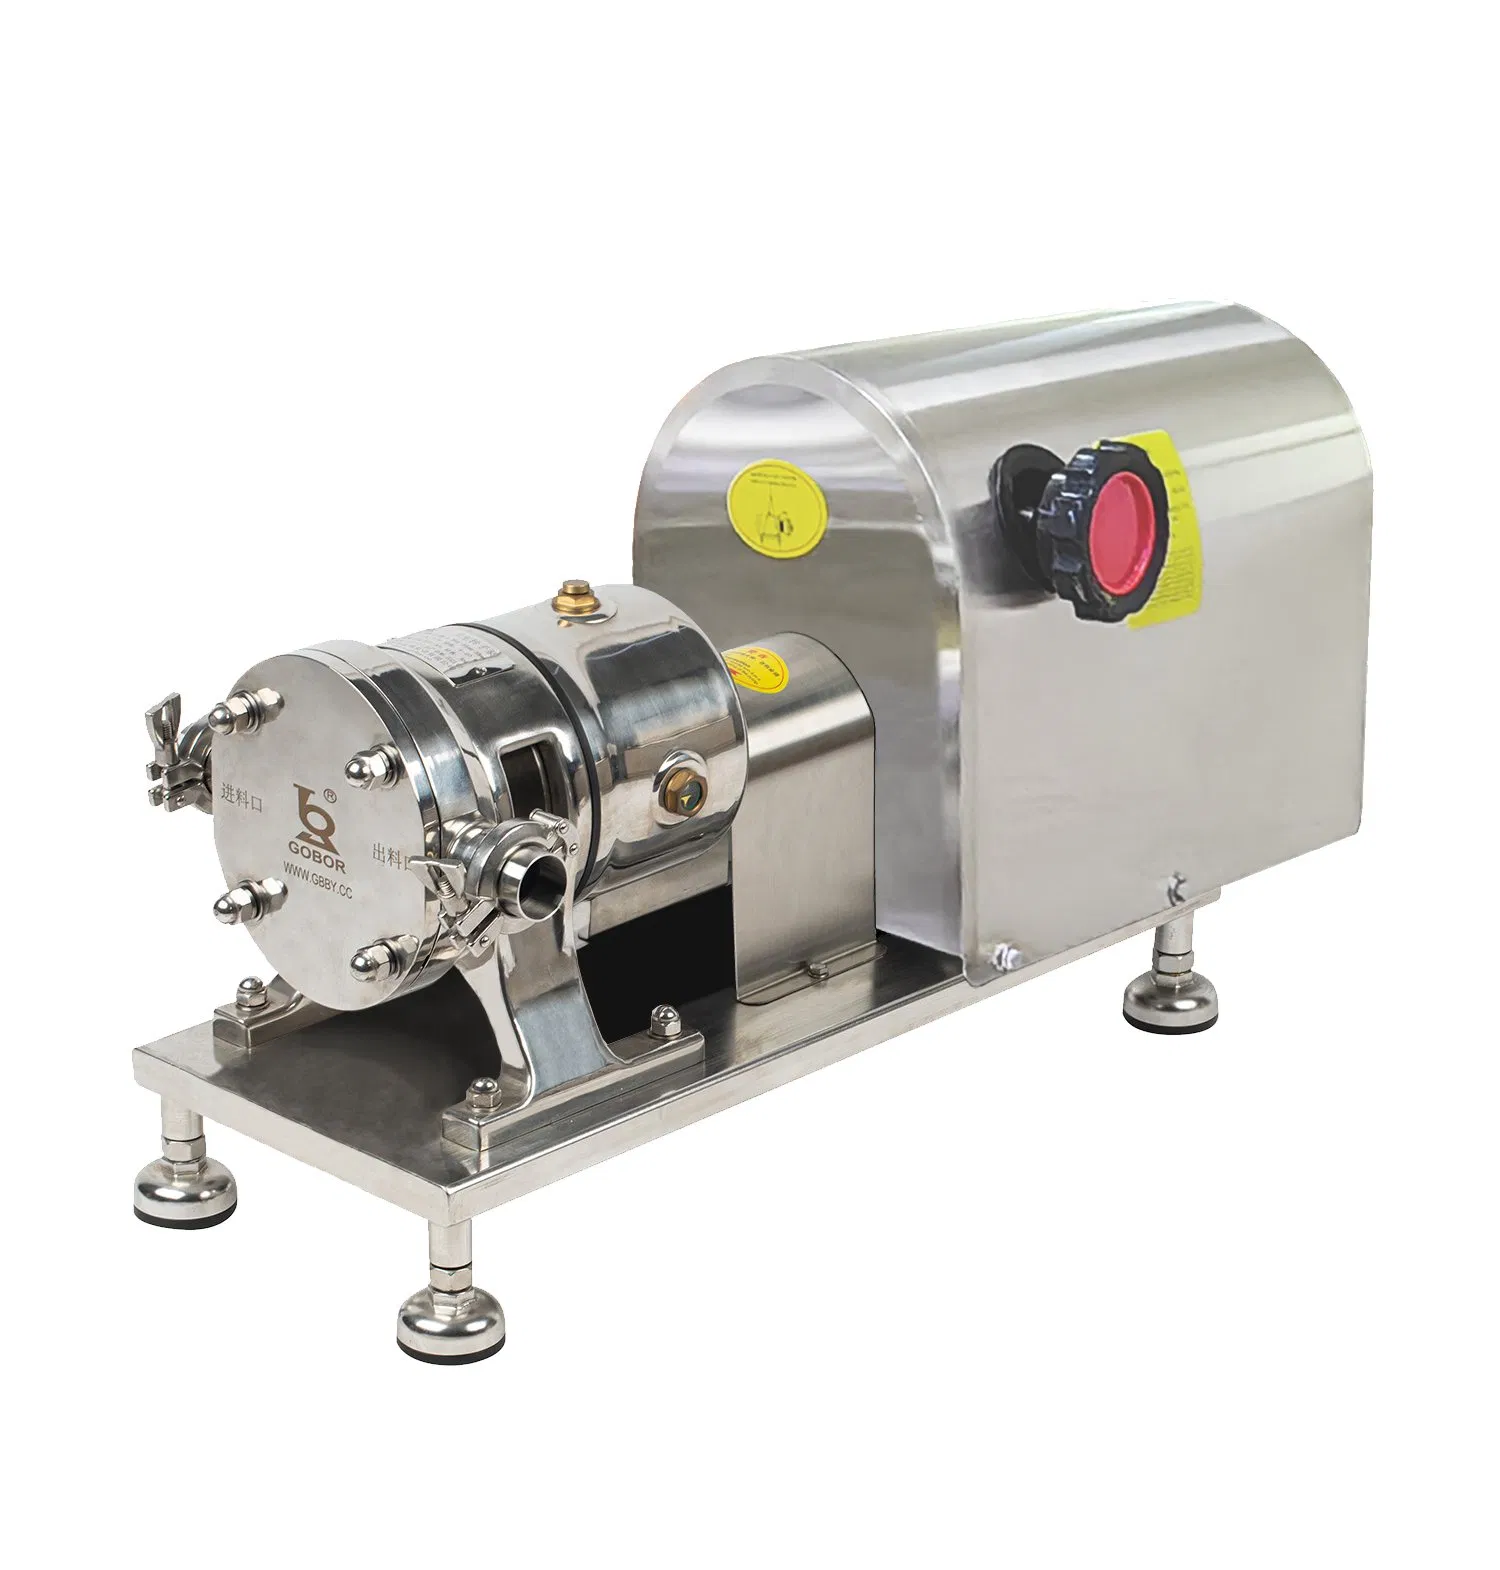
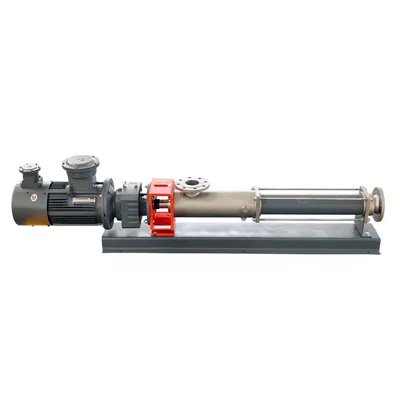
5t 2.2kw Rotor Pump/Lobe Pump for Chocolate Honey Heavy Liquid
4.0InStock Source-listed auditby Wenzhou Gaobo Pump Co., Ltd.
₹83,500≈ $1,000 · indicative, confirm with supplier
Payment
LC, T/T, D/P, PayPal, Western Union
Incoterms
FOB, CIF, CFR
Description
5t 2.2kw Rotor Pump/Lobe Pump for Chocolate Honey Heavy Liquid. Food Grade Sanitary Design: Suitable for chocolate, honey, dairy, and high-viscosity food transportation. Durable Mechanical Seal: Silicon carbide static ring and alloy dynamic ring with 316L spring support. Optional Customizations: Available with warm jacket, explosion-proof motor, vertical pipe, and discharge valve. Stable Lobe Pump Performance: Low flow pulsation, high carrying capacity, and improved volumetric efficiency. CE and ISO Certified: Manufactured by Wenzhou Gaobo Pump with ISO 9001 and CE certification. Factory Quality Testing: Each pump undergoes a 2-hour continuous start-up and pressure test before shipment. Versatile Application Range: Ideal for food, dairy, beer, cosmetics, and pharmaceutical industries. Efficient Vertical Pipe Option: Enables smooth gravity flow into the pump chamber for better operational stability.
Specifications
Warranty12 Months Guarantee
Model NO.GKR3-66-2.2kw-38
Screw NumberDouble Screw Pump
CustomizationAvailable
After-sales Service12 Months Guarantee